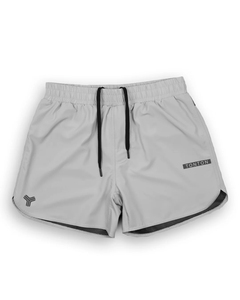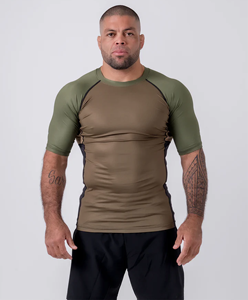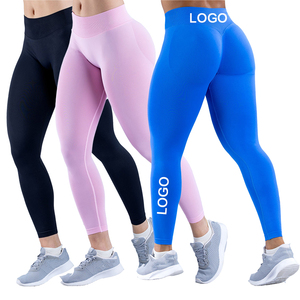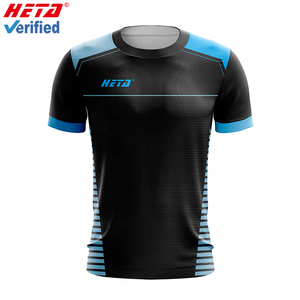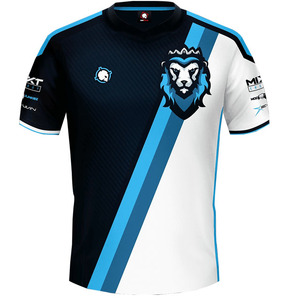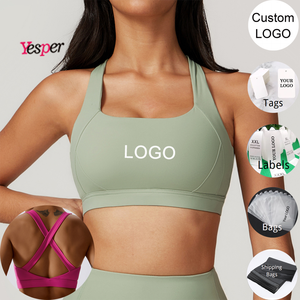
Curated technical silhouettes engineered with micro-filament disperse ink bonding, multi-directional elasticity, and flatlock anti-abrasion construction. Fully customizable via bespoke private label programs.
Analysis of macro supply-chain realignments, digital inventory optimization, zero dead-stock manufacturing, and environmental compliance frameworks for global sporting brands.
The global athletic teamwear procurement landscape is undergoing an aggressive structural migration away from traditional bulk container forecasts toward decentralized, demand-responsive supply chains. Institutional sports clubs, esports franchises, educational athletics, and direct-to-consumer (DTC) athletic apparel brands are re-engineering their supplier evaluation scorecards to prioritize rapid-cycle manufacturing velocity, micro-batch customization elasticity, and verifiable ESG compliance.
Procurement directors are actively reducing warehouse risk by switching to 20-50 piece initial pilot batches with automated replenishment. Digital sublimation workflows bypass traditional rotary screen charges, allowing teams to react to roster changes and seasonal wins in sub-10 day operational cycles.
Institutional procurement guidelines across Europe and North America increasingly require GRS (Global Recycled Standard) certified post-consumer recycled polyester. Sourcing executives now evaluate sublimation dye binders based on their degradation neutrality and ability to endure 50+ industrial wash cycles without VOC emissions.
Modern B2B buyers mandate full traceability from raw yarn knitting to final seam assembly. Leading sublimation factories now interface directly with brand ERP systems, offering automated real-time status notifications across pre-press sublimation rip, calender heat transfer, computer laser cutting, and QC audits.
| Procurement Dimension | Legacy Procurement Model (2015-2020) | Next-Gen Agile Sublimation (2025-2030) | Strategic Buyer Impact |
|---|---|---|---|
| Minimum Order Quantity (MOQ) | 500 - 1,000 units per colorway | 20 - 50 units (Full customization) | Eliminates 92% Inventory Dead-Stock |
| Production Lead Time | 45 - 75 working days | 7 - 14 working days | 4.5x Acceleration in Speed to Market |
| Color Reproducibility | Batch-dependent visually eyeballed dyes | Spectrophotometer ΔE < 0.8 digital calibration | Flawless Corporate Brand Identity |
| Fabric Technical Integrity | Generic 100% virgin polyester | GRS rPET, Anti-microbial, UPF 50+, Chitosan treated | Complies with Global Green Sourcing |
A deep dive into high-molecular dye-sublimation kinetics, thermal-diffusion polymer matrix bonding, and automated multi-ply laser registration systems.
Historically, dye-sublimation athletic apparel was constrained by coarse polyester weaves, stiff hand-feels, and white fabric grinning under maximum mechanical stretch. Modern Chinese technical teamwear manufacturing has superseded these limitations through the synthesis of ultra-fine filament micro-polyester yarns, high-solid disperse dye chemistry, and industrial multi-zone calender drums.
Unlike silkscreen or vinyl film printing which deposits rubberized plastisol layers on top of fabrics, sublimation transitions specialized inks directly from solid to gaseous states at 200°C. The gaseous dye permanently diffuses into the amorphous polyester macromolecular chains, guaranteeing zero degradation, zero cracking, and 100% natural breathability.
Traditional manual fabric shears introduce sizing deviances of 1.5cm - 3.0cm between panels. Automated optical vision laser cutters automatically compensate for dimensional fabric shrinkage post-calendering, matching vector boundary points with a tolerance of ±0.3mm, ensuring anatomical symmetry across jerseys and compression leggings.
High-friction team sports (rugby, MMA, wrestling, soccer) demand superior seam shear strength. Modern lines utilize Japanese-engineered 4-needle 6-thread flatlock machines that stitch low-profile, skin-chafing-free seams capable of withstanding over 180 Newtons of mechanical tensile force.
A completely integrated, unmediated OEM/ODM manufacturing facility delivering institutional accountability, technical rigor, and end-to-end proprietary quality controls.
You work directly with the manufacturing facility that cuts, sublimates, sews, and inspects your garments. Eliminating trading brokers yields 25%-35% direct cost recovery, instantaneous pattern engineering revisions, and uncompromised transparency.
We empower expanding apparel labels, university athletics, and boutique fitness clubs to deploy customized collections starting from just 20 pieces per design. Sizes, athlete names, and numbers can be seamlessly mixed without penalty surcharges.
Equipped with Epson PrecisionCore® and Mimaki® high-resolution output engines using certified European disperse inks. Custom Pantone, CMYK, and fluorescent lab-dips achieve an extraordinary precision delta of ΔE < 0.8 across repeat dye lots.
Every single unit undergoes an exhaustive 4-stage audit: pre-heat transfer print check, post-sublimation shrinkage audit, dynamic seam-pull tensile verification, and 100% finished-garment needle-detection and trim inspection before hermetic polybagging.
Transform raw silhouettes into full-scale retail collections. We produce custom-woven satin neck labels, high-density silicone heat seals, laser-cut hang tags with scannable QR/EAN barcodes, branded frosted polybags, and custom master shipping cartons.
Through established logistics agreements with DHL, FedEx, and international air/sea freight carriers, we supply doorstep DDP (Delivered Duty Paid) fulfillment to over 30 countries. Urgent tournament reorders are expedited through dedicated fast-track sewing lines.
Essential technical, commercial, and operational clarifications addressed directly by our senior production engineering staff.