
From moisture-wicking compression bases to waterproof micro-poly windbreakers, our export lines are rigorously tested to exceed international ISO 13934 tensile strength and AATCC 197 capillary moisture-management benchmarks.
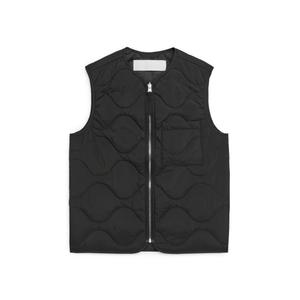
Ultra-lightweight micro-ripstop nylon with synthetic thermolite cluster fill, sealed wind baffles, and DWR finish suited for brisk coastal runs and athleisure styling.
View Specifications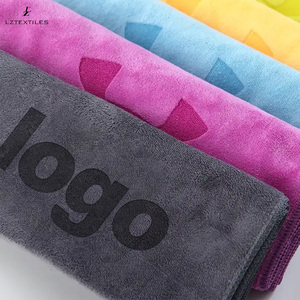
High-capillary split-microfiber fabric absorbing 400% dry weight, embedded antimicrobial zinc ions, and vibrant zero-handfeel sublimation branding.
View Specifications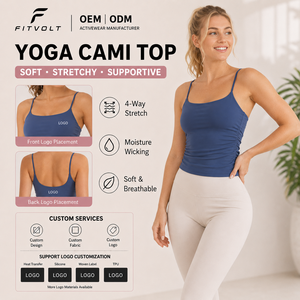
Circular-knit seamless elastane blend engineered with mapped ventilation ribs and removable memory cups, preventing skin chafing in humid workout conditions.
View Specifications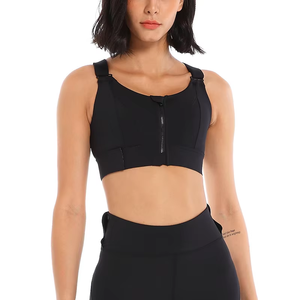
High-torsion 75D/40D interlock structure delivering 70% bounce reduction, front locking zipper with anti-pinch inner placket, and brushed moisture-wicking bottom band.
View Specifications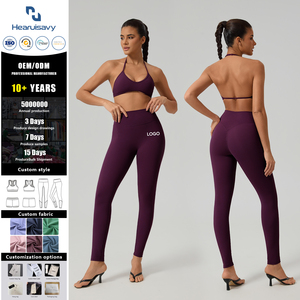
Buttery-soft 280 GSM brushed poly-spandex delivering 100% squat-proof opacity, contoured ruched posterior detailing, and bonded high-waist abdominal compression.
View Specifications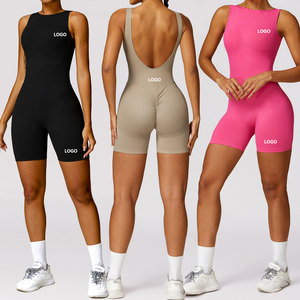
One-piece anatomic unitard incorporating flatlock ergonomic seam maps, four-way elasticity, and accelerated evaporation channels designed for hot Pilates and studio conditioning.
View Specifications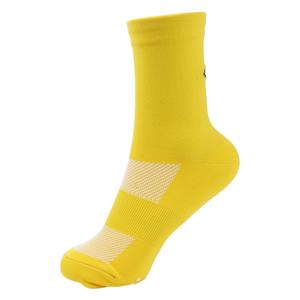
168-needle technical knit integrating graduated 15-20 mmHg plantar arch compression, COOLMAX moisture exhaust mesh instep, and reinforced terry friction pads.
View Specifications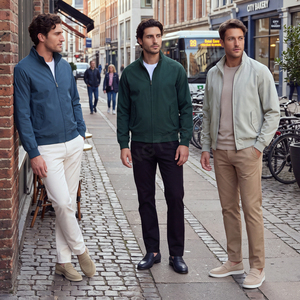
Durable water-repellent micro-weave softshell featuring underarm laser-cut ventilation eyelets, storm placket SBS zippers, and packable pocket configuration.
View SpecificationsNavigating coastal salinity, oppressive monsoon humidity exceeding 85%, and round-the-clock metropolitan agility requires textile engineering that transcends generic market catalog blanks.
From premium boutique pilates hubs in Bandra West and Juhu to high-density CrossFit boxes in Lower Parel, Mumbai athletes battle non-evaporative ambient sweat saturation. Our 4-way stretch fabrics incorporate micro-filament channel yarns that pull sweat laterally across an extended surface area, accelerating drying times by 48% over standard cotton blends.
Mumbai's Southwest monsoon inundates the Western Line and corporate corridors from Nariman Point to BKC. Active professionals demand outerwear with hydrostatic water head ratings of 5,000mm to 10,000mm combined with microporous breathability. Our packable windbreakers and ripstop nylon vests deliver waterproof shielding without inducing internal sauna effects.
With the iconic Marine Drive promenade, Bandstand, and Shivaji Park hosting dawn running clubs and annual Tata Mumbai Marathon training squads, anti-friction and salt-tolerance are paramount. We construct our bottoms and compression tops with flatlock 4-needle 6-thread stitching using bonded micro-nylon threads to prevent chaffing caused by dried saline sweat crystallization.
India's commercial powerhouse is undergoing a transformative athletic wear revolution. Direct-to-consumer (D2C) brands, fitness influencers, and athletic academies are re-architecting supply chains toward agile manufacturing.
Mumbai's consumer base is abandoning unbranded street-market cotton activewear in favor of luxury gymwear labels that rival Lululemon and Gymshark. D2C founders require premium matte nylon-spandex blends and custom-molded silicone hardware.
Bacterial proliferation is an intrinsic hazard of Mumbai's prolonged humidity. Local corporate wellness programs and fitness chains mandate activewear with embedded silver-ion and zinc pyrithione finishes certified to retain 99% efficacy after 50 wash cycles.
Eco-conscious consumer sentiment across Mumbai suburban centers has elevated demand for Global Recycled Standard (GRS) certified polyester, derived from recycled post-consumer bottles and ocean-bound plastics without compromising tensile durability.
Traditional seasonal bulk commitments (6-month lead times) are obsolete. Mumbai retail curators operate on rapid 6-week micro-capsule drops, necessitating flexible OEM factory setups that support low-MOQ test batches before scaling commercial volume.
Headquartered in Sialkot, Pakistan—the globally recognized manufacturing epicenter producing over 40% of the world's performance sports goods—ALEZ Industry operates a vertically integrated industrial complex. By sourcing directly with us, Mumbai apparel brands eliminate third-party domestic middlemen, agents, and trading houses that inflate landed costs by 30% to 50%.
Our complete production cycle is managed under one roof: from computerized CAD grading and automated laser fabric cutting to multi-head Tajima embroidery, industrial Italian sublimation printing, and strict ISO-aligned quality verification checkpoints.
Every bulk shipment destined for Mumbai or the Jawaharlal Nehru Port (JNPT) is pre-qualified against approved golden pre-production samples, ensuring needle-to-needle compliance in GSM, dimensional stability, and colorfastness.

Compare our proprietary athletic textile formulations engineered to withstand coastal humidity, daily commercial washing, and extreme physical exertion.
| Fabric Nomenclature | Composition & Weight | Textile Properties | Optimal Mumbai Application |
|---|---|---|---|
| AeroWeave™ Interlock | 85% Micro-Polyester / 15% Spandex (220 GSM) | Capillary moisture wicking, 4-way stretch, UPF 50+ UV filter | Running singlets, outdoor training tees, cycling apparel |
| LuxeSculpt™ Double-Knit | 75% Polyamide (Nylon 6.6) / 25% Spandex (280 GSM) | Matte peach-skin handfeel, squat-proof opacity, zero pilling | High-waist yoga leggings, compression tights, sports bras |
| HydroShield™ Ripstop | 100% High-Tenacity Micro Nylon (110 GSM) | DWR micro-coating, windproof, tear-resistant, breathable film | Monsoon track jackets, ultra-light windbreakers, shell vests |
| ThermoGrid™ Fleece | 92% Polyester / 8% Elastane (310 GSM) | Brushed grid backing for thermal regulation and airflow venting | Gym warmup pullovers, airport travel hoodies, travel sets |
We fuse precision artisanal tailoring with high-volume industrial capability, unlocking superior unit economics for our international partners.
Launch novel designs without tying up working capital in thousands of stagnant units. Our modular manufacturing cells accommodate test orders from just 20 pieces per design, allowing scalable size breakdowns across XS to 3XL.
We eliminate uncertainty before mass cutting begins. A full physical sample complete with your bespoke heat-transfer tags, woven neck labels, and custom hardware is delivered to your office for tactile fit approval.
Get real-time line-item transparent bill of materials (BOM) quotations within 24 hours. Clear breakdowns for yarn weight, decoration, trims, and packaging eliminate hidden surprise surcharges.
Complete unboxing branding: high-definition woven neck labels, matte silicone heat transfers, custom soft-touch TPU zipper pullers, GS1 barcode sticker tags, and frosted biodegradable polybags ready for Mumbai distribution centers.
Comprehensive door-to-door delivery coverage serving Mumbai, Navi Mumbai, and Thane through global air couriers (DHL, FedEx) with 4-6 business days transit, or high-tonnage ocean container freight docking directly at JNPT (Nhava Sheva).
Unlike trading agents who conduct random 5% spot checks, our dedicated quality control inspectors verify every single finished garment for seam tension, dimensional tolerance (+/- 1cm), color fastness to perspiration, and hardware durability.


Clear, definitive operational guidance regarding import clearances, fabric certifications, shipping routes, and payment structures.
Bulk air cargo arrives via Chhatrapati Shivaji Maharaj International Airport (BOM), while Full Container Load (FCL) or Less than Container Load (LCL) shipments arrive at JNPT (Nhava Sheva). We provide full standardized commercial invoices, packing lists with net/gross weights, HS codes (Chapter 61 & 62 for knitted/woven apparel), and Certificates of Origin. Your authorized Custom House Agent (CHA) utilizes your valid Import Export Code (IEC) to file the Bill of Entry on the ICEGATE portal.
Following approval of your golden pre-production sample, bulk production runs of 100 to 1,000 units are completed in 7 to 10 working days. Large commercial runs exceeding 5,000 units require 12 to 15 working days. Pre-production sampling generally requires 5 to 7 days plus courier delivery.
Yes. We offer precise Pantone Matching System (PMS) color dyeing on all our synthetic and natural fabrics. For custom-dyed batches, our dyehouse generates physical lab-dip swatches (A, B, C options with light-box verification under D65 daylight) for client sign-off prior to bulk mill knitting.
During the humid maritime transport cycle, moisture damage is a real threat. We package each garment in sealed, ventilated moisture-barrier polybags containing food-grade silica gel desiccant packs. Outer master cartons are reinforced 7-ply corrugated craft paper, shrink-wrapped, and seam-taped to eliminate ambient moisture ingress during port handling.
Standard production terms are a 70% advance deposit to initiate dedicated fabric allocation, pattern cutting, and production line scheduling, with the remaining 30% balance plus freight settled upon final quality inspection approval prior to factory dispatch. We accept secure Swift Wire Transfers (TT), PayPal, Payoneer, and Wise.
Absolutely. We specialize in high-gauge 28-gauge to 32-gauge knitting machines utilizing high-elastane (20% to 28% Spandex) double-knit interlocks ranging from 260 GSM to 320 GSM. Each batch undergoes multi-directional elongation stretch and lux-meter light transmission testing to ensure zero transparency in deep squats.
Connect directly with our senior production engineering team. Receive detailed line-item costing, complimentary digital mockups, and fabric recommendations tailored to your brand's technical specifications within 24 hours.
Contact Us