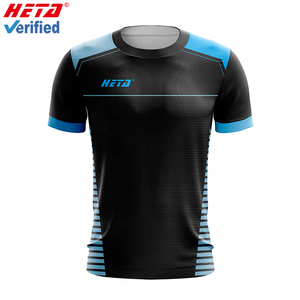
Direct-from-factory technical sportswear manufactured by ALEZ Industry. Built with high-tenacity polyester filaments, ergonomic micro-ventilation, and high-density sublimated pigment integration.
A comprehensive analysis of textile thermodynamics, sub-tropical playability, and international compliance requirements for professional and grassroots cricket in Kanto, Kansai, and beyond.
The operational landscape of custom team sportswear in Japan has entered an era of technical differentiation. Unlike conventional baseball or soccer apparel lines, custom cricket uniforms face a multifaceted biomechanical and environmental demand profile. Cricket requires prolonged cardiovascular activity combined with sudden, explosive kinematic bursts (bowling delivery strides, boundary sprints, dynamic sliding stops). These activities occur outdoors over 3 to 8 hours under intense direct solar exposure. For institutional leagues, corporate teams, and university clubs spanning the Kanto Cricket League, the Japan Premier League (JPL), and regional hubs such as Sano City, the textile specification must address distinct heat dissipation challenges while conforming to strict aesthetic and anti-abrasion criteria.
As a vertically integrated original equipment manufacturer (OEM) and original design manufacturer (ODM) based in Sialkot, Pakistan—supported by direct corporate representation across North America and Tokyo, Japan (led by Representative Sheikh Nisar)—ALEZ Industry bridges the manufacturing legacy of Punjab’s world-renowned sports industrial cluster with Japanese procurement protocols: absolute defect elimination, colorfastness across repeated wash cycles, and adherence to environmental compliance under JIS standards.
Engineered using hollow-core micro-filament polyester fibers (140–160 GSM) that transport perspiration away from the skin via micro-capillary channels, drying up to 3.2 times faster than conventional double-knit cotton blends during Japanese summer play.
Utilizing high-purity, environmentally certified Italian sublimation inks, colors cross the molecular threshold into the polymer matrix at 205°C. Logos, team crests, and corporate branding retain clarity without peeling, cracking, or blocking airflow.
Cricket trousers and boundary-fielding jerseys feature flatlock 4-thread overlock seam construction with localized bartack reinforcement at critical tensile stress junctions, preventing seam failures during deep crouches and dives.
How technical tailoring meets the specific physical conditions of turf wickets, multi-use grounds, and regional climatic shifts across Japan.
The expansion of cricket across Japan presents distinctive operational parameters that standard catalogue uniforms fail to resolve. Ground usage policies, synthetic artificial turf abrasion, and the intense humidity of the Japanese summer require precise, fit-for-purpose adjustments:
At regional centers such as the Sano International Cricket Ground, synthetic hybrid pitches and dry clay outfields require trousers with elastane-reinforced knee gussets to prevent fabric burns and snagging during dives.
Between late June and August, ambient relative humidity frequently exceeds 80%. Our Japanese line utilizes jacquard-weave mesh side panels and quick-dry hydrophobic yarn to mitigate fabric cling and reduce player thermal strain.
Teams from institutions like Waseda, Keio, and multinational tech leagues demand streamlined, ergonomic sizing ("Slim-Pro Athlete Cut") rather than standard Western sizing, ensuring snug fitting that prevents equipment interference.
| Performance Vector | ALEZ Precision Custom Uniforms | Generic Domestic Reseller | Standard Low-Cost Export |
|---|---|---|---|
| Fabric Composition | 100% Micro-Filament Interlock / Spandex blend (160 GSM) | Stock 100% Polyester Mesh (130 GSM) | Regenerated Mixed Poly-Cotton |
| UV Solar Protection | Certified UPF 50+ (Blocks 98% UVA/UVB) | Unrated (Typically UPF 15–20) | No protective barrier |
| Seam Strength (Tensile) | 4-Needle Flatlock with Cordura-reinforced knee panelling | Basic 3-Thread Overlock | Single-needle chain stitch (prone to runs) |
| Sublimation Colorfastness | Level 4.5+ (JIS L 0844 compliant across 50 wash cycles) | Level 3 (Visibly fades under direct sun) | Level 2 (Bleeds into light panel fabrics) |
| Minimum Order Quantity | 20 Pieces (Mixed sizing & individual player names) | 50–100 Pieces (Fixed package pricing) | 100+ Pieces with limited customization |
Direct-to-factory transparency without intermediary markups. Cut, printed, stitched, and inspected under comprehensive quality control protocols.
Historically, sports equipment buyers in Japan paid inflated prices through regional trading companies (*shousha*) or regional third-party agents who outsourced manufacturing to factories across South Asia. ALEZ Industry eliminates these supply layers by granting direct factory access to athletic directors, league commissioners, apparel founders, and sporting federations.
Operating from our modern production hub in Bismillah Chowk, Pasrur Road, Sialkot, our facility houses CAD-driven laser cutting tables, a dedicated 12-head industrial embroidery setup, wide-format high-speed sublimation printers, and clean finishing assemblies. Because sports manufacturing runs through Sialkot’s industrial core—supplying over 40% of the world's competitive athletic equipment—our mill access provides custom-milled textiles, high-tenacity core threads, and tailored hardware within days.
With corporate representation in Japan headed by Sheikh Nisar, your operations enjoy bilingual technical consultations, rapid pattern sample deliveries, flexible Japanese Yen/USD transaction options, and transparent logistics through reliable air and maritime carriers.
Essential guidance on minimums, Japanese sizing standards, customs clearance, and sample auditing protocols.
We work directly with Japanese sizing specifications (JIS L 4004/4005). Standard Western cuts are often broad across the chest and shoulders for Asian athletes. We construct customized patterns—narrowing the torso profile, raising armhole drops, and tailoring sleeve length for an optimal athletic fit.
Our baseline factory MOQ is strictly 20 pieces per design. You can split these 20 units across multiple sizes (S, M, L, XL, 2XL) and assign individual player roster names and numbers via digital sublimation printing at no additional setup surcharge.
Yes. After your vector artwork or tech pack is reviewed, we produce a complete physical pre-production sample jersey/trouser set within 5 to 7 business days. We dispatch this directly to your address in Tokyo, Osaka, or elsewhere via express air freight for inspection.
We provide commercial invoices, packing lists, and Certificates of Origin (COO) under relevant international trade classifications (HS Code 6103 / 6104). We partner with major air couriers (DHL Express, FedEx, UPS) to ensure seamless customs clearance through Narita or Kansai International Airport.
We utilize digital dye sublimation for full-color patterns and complex sponsor logos. Unlike surface heat transfers, dye sublimation vaporizes reactive ink pigments directly into the polyester filament structure under heat and pressure, ensuring logos never peel, crack, or wash away.
Our standard terms involve a 70% production advance to reserve factory capacity, initiate custom knitting, and start cutting lines, with the remaining 30% balance plus freight settled upon final photo inspection before dispatch. We accept Wire Transfers, PayPal, Wise, and Payoneer.