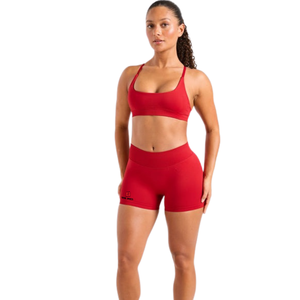
Women's High Waist Biker Shorts Workout Gym Training Moisture Wicking
Designed for female basketball rosters and strength sessions. High-tension interlock knit prevents ride-up during aggressive lateral defensive slides.
Engineered for Boston's winter humidity differentials and intensive high-contact hardwood play, our product portfolio combines high-tensile four-way stretch fibers, moisture-wicking capillary yarns, and cold-weather bench insulation.
Designed for female basketball rosters and strength sessions. High-tension interlock knit prevents ride-up during aggressive lateral defensive slides.
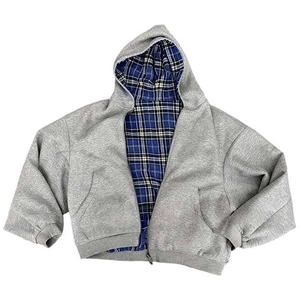
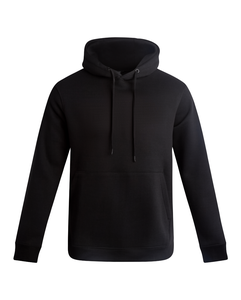
Built for New England travel schedules. Heavyweight fleece lined with brushed thermal flannel maintains player core temperature between hotel and arena.
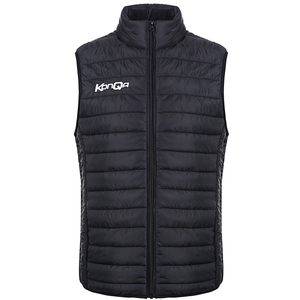
Ergonomic armhole cut allows unrestricted clipboard signaling and mobility for coaching staff during draughty fieldhouse tournament weekends.
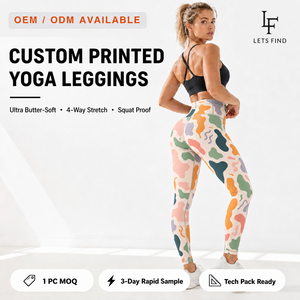
All-over sublimation that preserves fiber elasticity without cracking or transparency. Used as baseline warmup tights and athletic retail merchandise.
Engineered for pre-tipoff shootarounds. Poly-fleece thermal construction traps convective warmth while venting perspiration through underarm gussets.
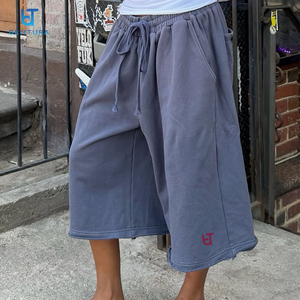
Drop-crotch, breathable French terry knit engineered for heavy plyometric jumping and recovery conditioning. Deep pockets fitted with hidden zippers.
High-pile ring-spun yarn absorbent court towels. Custom jacquard woven club branding that withstands commercial institutional chlorination washes.
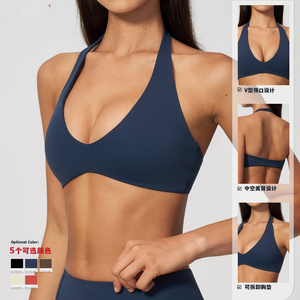
High-compression underbust band stabilizing multi-directional breast displacement during fast-break transitions. Perforated cup linings expel moisture.
For decades, athletic directors across the Greater Boston area—from NCAA Division I and Division III athletic programs along Commonwealth Avenue to elite AAU travel networks competing at Spooky Nook and regional New England complexes—have operated within an inefficient, high-markup brokerage paradigm. Domestically warehoused basketball uniforms frequently travel through as many as three intermediaries before reaching the athletic equipment cage: overseas CMT factories, multinational wholesale distributors, regional embellishers, and local sporting goods dealers.
This redundant supply chain inflates per-uniform acquisition costs by 180% to 260%, mandates six-to-ten-week lead windows, and leaves coaching staffs vulnerable to abrupt mid-season stock-outs when a sudden roster addition or damaged jersey requires replenishment. ALEZ Industry dismantles this intermediary drag. Operating out of Sialkot, Pakistan—a global manufacturing cluster responsible for over 40% of premier international sports gear—we deliver direct OEM & ODM production capabilities directly to the Boston market.
With an operational footprint overseen by international client representatives—including Johnny Johnson in the United States—we bridge the geographic distance between South Asian high-precision textile mills and New England tournament courts, ensuring rapid technical communication, sample-first prototyping, and end-to-end cargo visibility.
100+ Master Craftsmen
Boston Logan (BOS) Air Cargo Express
The New England basketball ecosystem is diverse, demanding garments that transition seamlessly from heated hardwood arenas to zero-degree transit terminals. Here is how our custom apparel architecture solves local programmatic challenges.
Greater Boston hosts one of the dense collegiate concentrations on Earth, featuring institutions across the ACC, America East, Patriot League, and NEWMAC conferences. Varsity basketball demands compliance with stringent NCAA uniform bylaws regarding number legibility, neutral-zone contrast, and manufacturer logo sizing.
Our sublimation jerseys incorporate interlock micro-mesh (150–160 GSM) that yields zero color bleeding under sweat deluge, maintaining high-definition visual separation on high-speed sports broadcasts.
From the Massachusetts Youth Basketball Association to spring Nike EYBL / Adidas 3SSB qualifiers, AAU programs face punishing back-to-back tournament schedules where rosters play four to six games within 48 hours.
Standard screen-printed jerseys crack and peel after repeated institutional laundering. Our deep-infusion sublimation embeds water-based Italian dyes directly into poly-elastane fibers at 210°C, guaranteeing uncrackable numbers, names, and gradient sponsors.
From Kendall Square biotechnology firms and Financial District investment banks to the Boston Parks and Recreation community adult leagues, recreational rosters demand premium aesthetic appeal without professional-franchise cost barriers.
With our 20-piece MOQ, local organizers can produce bespoke, fully branded uniforms that outperform standard generic off-the-shelf blanks, complete with custom sublimation patterns, team mascots, and custom silicone waistbands.
In basketball apparel procurement, textile weight, hydrostatic breathability, and seam tensile limits dictate court longevity. Review the technical breakdown powering our uniform assemblies.
| Performance Parameter | ALEZ Full-Dye Sublimation Knit | Traditional Heavy Tackle Twill | Off-the-Shelf Screenprinted Blanks |
|---|---|---|---|
| Fabric Composition & Weight | 150–165 GSM 100% Recycled Poly-Birdseye Mesh Optimal | 220–280 GSM Heavy Double-Knit Dazzle | 130–140 GSM Standard Tubular Jersey |
| Moisture Management (Capillary Wicking) | Instant vapor dissemination (<1.8s absorption) | Slow drying; sweat accumulates in twill patches | Moderate; print blocks sweat evaporation |
| Weight Under Sweat Saturation | Increases <14% dry weight | Increases 45%–65% dry weight (player fatigue factor) | Increases 22%–30% |
| Graphics & Number Durability | Molecular dye fusion: Zero fading, cracking, or peeling Lifetime | High durability, but perimeter embroidery threads can snag | Cracks and peels after 12–18 institutional washes |
| Boston Cold Transit Versatility | Pairs seamlessly beneath 380 GSM fleece shooting pullovers | Bulky; causes friction chafing under winter hoodies | Inconsistent sizing across brand dye lots |
| Minimum Production Run (MOQ) | 20 Pieces (mix size ratios freely) Factory Direct | 50–100 Pieces minimum | Variable, but personalization adds heavy fees |
Four-Thread Overlock Reinforcement
Pantone Formula Solid Coated Matching
Procurement teams across Massachusetts are discarding legacy catalog ordering in favor of specialized, data-driven apparel sourcing. Four definitive trends dominate purchasing meetings for the upcoming competitive seasons:
1. The Rise of Anthropometrically Accurate Women's Patterning: Historically, female basketball programs received unisex (scaled-down men's) uniforms resulting in uncomfortable fits, oversized armholes, and waistline slipping. ALEZ Industry engineers dedicated female cuts characterized by narrower shoulder aprons, tailored chest contours, and sports-bra concealing arm openings.
2. Recycled Poly (rPET) Mandates: Greater Boston educational boards and progressive independent academies increasingly demand verified eco-responsible textiles. We provide recycled polyester yarns synthesized from post-consumer plastics, matching the tensile strength and breathability of virgin polymers while lowering program carbon footprints.
3. Comprehensive "Sideline to Hardwood" Uniform Systems: Programs no longer purchase disconnected singlets. They require integrated collections combining game jerseys, compression base-layers, plaid-lined travel hoodies, and bench puffer vests with identical Pantone branding and typography.
Our standardized manufacturing checkpoints ensure zero discrepancy between your art proof and delivered bulk uniforms.
Submit your tech pack, roster list, or hand sketch. We translate artwork into production-ready pattern templates across adult, youth, and women's dimensions.
Direct-from-plant pricing returned within 24 business hours, providing detailed fabric options, embellishment styles, and transit freight breakdowns.
Secure production queue booking with standard terms (70% advance, 30% balance upon dispatch). Digital Pantone lab-dip color simulations approved before cutting.
We produce a physical sample uniform jersey. High-res macro imagery or rapid DHL air express delivery ensures total tactile confidence before bulk activation.
Computerized laser cutters seal polyester fabric edges to prevent fraying. 210°C high-vacuum heat calendar transfers sublimated graphics with absolute saturation.
Industrial stitching lines utilize elastic 4-thread overlock and safety seams, ensuring tensile tolerance against high-contact defensive clutching.
Every jersey and short is hand-measured against sizing charts, verified for spell-check, and stress-tested at all load points before polybag sealing.
Consignments clear through US Customs with automated tracking delivered directly to your school, campus athletics cage, or corporate headquarters in Boston.
Combining heritage South Asian textile craftsmanship with modern Western business accountability.
We are a 100% direct manufacturer with our own manufacturing facility located at Bismillah Chowk, Pasrur Road in Sialkot. No middlemen, no domestic re-sellers, and no hidden commission fees.
While legacy overseas factories demand 500-unit commitments, ALEZ Industry supports agile programs with a low 20-piece MOQ per design—allowing you to order only what your roster demands.
Our domestic representation headed by Johnny Johnson in the United States guarantees same-timezone communication, streamlining quotes, logistics, and rapid question resolution.
Orders under 1,000 units require only 7 to 10 working days for production following sample approval. Larger multi-team programs complete within 12 to 15 days, easily beating domestic broker timeframes.
Elevate your club with custom woven interior neck labels, heat-transfer wash tags, laser-cut silicone badges, and branded packaging cartons suitable for retail and boosters.
Our facility welcomes international buyers and third-party compliance auditors. Every batch conforms to international labor regulations and strict non-toxic dye chemistry protocols.
Straightforward answers addressing turnaround schedules, compliance, fabric durability, and payment security.
We engineer uniforms following standard NFHS (National Federation of State High School Associations), MIAA (Massachusetts Interscholastic Athletic Association), and NCAA uniform specifications. This includes guaranteed 4-inch minimum front number height, 6-inch back number height, proper neutral torso contrast zones, correct single manufacturer logo positioning (under 2.25 square inches), and compliant referee-visible color contrast borders.
Following physical sample approval, standard manufacturing for 20 to 500 team uniforms requires 7 to 10 working days. We then ship via priority international air express (DHL / FedEx Express / Air Cargo) directly into Boston Logan International Airport (BOS) or local distribution centers, taking 4 to 6 transit days. The entire cycle from digital proof to campus delivery typically averages 16 to 22 business days.
Yes. Unlike domestic distributors that discontinue uniform lines yearly or refuse orders beneath heavy minimums, ALEZ Industry archives your digital sublimation vector profiles, Pantone lab formulations, and cutting patterns indefinitely. When a Boston program needs 2 replacement jerseys for new recruits or damaged kit, we reproduce them at factory pricing without requiring a new full-team bulk order.
We do not use generic guessing. We formulate inks strictly against the Pantone Matching System (PMS Formula Solid Coated). We conduct lab-dip color strike-offs on the specific polyester mesh blend selected for your team, ensuring that Harvard Crimson (Pantone 201 C), Boston College Maroon (Pantone 202 C), or classic Celtics-style green (Pantone 356 C) match your university brand standards precisely.
We accept official Institutional Bank Wire Transfers (TT), PayPal, Payoneer, Wise, and Western Union. Standard production terms are 70% advance to initiate fabric mill sourcing and printing lines, with the remaining 30% plus air courier freight payable upon final photographic and video inspection approval prior to dispatch.