Pro Cycling Wear
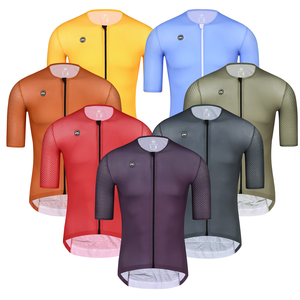

Direct factory production lines specializing in high-gauge circular knitting, compressive support, laser bonding, and sublimated athletic apparel manufactured for global athletic labels and fitness gym networks.
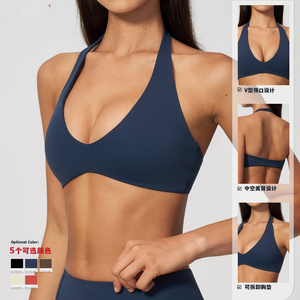
Sports bras are universally acknowledged across the apparel industry as the most complex garment to engineer in the activewear category. Combining three-dimensional breast biomechanics, thermal equilibrium, multidirectional kinetic load reduction, and skin-contact ergonomics requires millimeter-accurate pattern engineering and disciplined material science.
Uncontrolled vertical and lateral movement can cause permanent strain on Cooper's ligaments during intense athletic activity. Our factory utilizes dynamic breast displacement models to engineer dual-phase encapsulation and compression architectures. By anchoring the lower underbust band with engineered 38mm-45mm brushed elastane filaments, we restrict resonant oscillations by up to 78% without compromising vital tidal respiratory expansion during peak VO2 workouts.
The standard polyester blends prevalent in budget manufacturing are prone to chafing, pilling, and persistent moisture retention. We deploy premium 220–320 GSM 6.6 micro-denier Interlock Polyamides blended with Invista Lycra® or high-modulus elastane. This creates an exceptionally smooth surface, zero-friction skin interface, high puncture tear resistance, and rapid capillary moisture evacuation that keeps athletes cool under rigorous friction zones.
Traditional cut-and-sew methods introduce thick perimeter seams that irritate thoracic nerve endings and degrade under high tension. By harnessing specialized SANTONI circular knitting machines, we weave multi-zoned tension panels into a unified fabric tube. Tight compressive weaves stabilize the central sternum, while porous diamond mesh knit structures run along the spinal channel for immediate heat dispersion.
| Performance Parameter | Commercial Grade (Fast Fashion) | Our OEM Technical Standard | Brand Advantage |
|---|---|---|---|
| Displacement Attenuation | Single-ply compression (<35% bounce reduction) | Dual-layer encapsulated dynamic stabilization (>72% reduction) | Certified high-impact label status for running, HIIT, & crossfit. |
| Elastane Degradation | Standard spandex degrades after 25 wash cycles | Chlorine & sweat-stabilized Invista Lycra® (100+ wash rated) | Virtually zero stretch fatigue, minimal consumer returns for sagging. |
| Seam Integrity | Standard overlock seam (chafes sensitive skin) | Ultrasonic laser bonded edges + 4-needle 6-thread flatlock | Frictionless finish with true zero-chafe athletic compliance. |
| Cup Padding Engineering | Cheap polyurethane foam (folds and clumps) | Perforated high-resilience memory EVA (breathable, anti-shift) | Maintains anatomical contour post-wash; rapid dry aeration. |
International sports apparel procurement is evolving from high-volume speculative bulk purchasing to hyper-responsive, demand-driven sourcing. B2B buyers must adapt to five structural macro shifts to secure healthy profit margins and protect inventory liquidity.
Long lead times of 120 days are becoming obsolete. Contemporary D2C brands launch with test runs of 20 to 100 units per colorway, validate customer feedback via social platforms, and trigger rapid 10-day replenishment runs.
European and North American customs authorities are enforcing strict supply chain traceability. Global buyers now require GRS-certified recycled ocean plastics (rPET), bio-based nylon derived from castor oil, and OEKO-TEX Standard 100 Class I certifications.
Traditional stitch lines are being replaced by seamless thermofused adhesive films (Framis Italia). Premium brands favor cleanly bonded necklines and laser-cut underarms for minimalist aesthetics and pure second-skin comfort.
Physical sampling cycles are shifting to 3D virtual fitting simulations using CLO3D. Brands approve drape, tension strain maps, and colorways digitally, cutting pre-production lead times from 4 weeks down to 72 hours.
At our advanced manufacturing facilities, activewear production is treated as dynamic human bio-mechanics. Explore our specialized engineering systems that elevate basic wholesale apparel into premium high-tier athletic gear.
By blending hydrophilic micro-polyamide on the interior contact face with hydrophobic micro-polyester filaments on the outer shell, we generate a mechanical moisture gradient. Sweat is pulled away from the athlete's skin to the exterior surface in less than 0.8 seconds, eliminating post-workout chills and reducing bacterial colonies that cause fabric odors.
Disposable foam bra inserts that curl or crease in commercial laundry cycles cause widespread consumer frustration. Our factory utilizes high-heat hydraulic compression to mold permanently structured, non-migrating memory foam pads with micro-perforations. These ensure consistent chest modesty, breathability, and structural cup stability that endures over 100 laundry cycles.
Different regions of the upper torso require distinct levels of physical support. Our multi-zone circular knits integrate high-modulus compression bands along the inframammary fold for reliable lift, medium-modulus lateral slings to restrict outward drift, and low-modulus micro-mesh wings over the scapula for natural rotational shoulder mobility.
Combining generations of athletic apparel craftsmanship with high-throughput modern manufacturing equipment, we deliver uncompromised quality, low barrier-to-entry order thresholds, and end-to-end transparent supply chain oversight.
Traditional manufacturers turn down small production batches, forcing brands into risky inventory commitments. We support emerging labels and established teams by accepting customized runs from just 20 pieces per design, allowing you to validate fits, colorways, and markets without tying up working capital.
Eliminate middleman margins, broker markups, and delayed telephone games. You communicate directly with our in-house pattern-makers, sample technicians, and production directors. Decisions on tech-pack alterations, pantone lab dips, and packaging take hours instead of weeks.
With operational facilities in Sialkot, dedicated China raw-material sourcing hubs, and liaison representatives situated in the United States and Japan, we bridge the gap between Asian production power and Western quality standards. We offer complete DDP, air courier, and ocean freight logistics to over 30 countries.
Full CAD grading, stitch allocation, and elasticity calculation analyzed within 24 hours.
Pantone cotton-swatch matching, stretch recovery tests, and GSM verification.
Physical sample shipped directly to your desk for fit check, padding review, and sign-off.
Automated CNC fabric cutting ensuring sub-millimeter precision across every panel.
Tensioned sewing lines utilizing 4-needle 6-thread machinery and reinforced bar-tacking.
100% individual garment inspection for stitch tensile strength, cup symmetry, and measurements.
Custom woven neck tags, hang tags, barcoded SKU bags, and presentation mailers.
Express courier (DHL, FedEx, UPS) or freight forwarders with full tracking straight to your warehouse.
Clear, direct answers regarding minimum quantities, international testing benchmarks, custom molding, sample timelines, and payment security.
Whether you are launching a specialized compression bra line from 20 pieces or scaling high-volume retail activewear programs, our engineers provide complete costings, pattern grading, and physical prototypes within 24 hours.