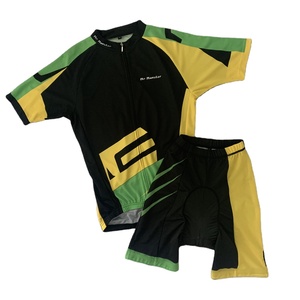
Engineered with zero-friction flatlock stitching, active moisture-wicking textiles, and industrial high-density sublimation printing for competitive field supremacy.
How cutting-edge supply chains deliver quantifiable commercial ROI, ultra-durable textiles, and agility for modern club leagues and international sportswear brands.
Modern baseball demands rigorous abrasion tolerance against high-velocity slides and repetitive torque motions. Advanced exporters utilize 220–260 GSM warp-knit polyester integrated with four-way mechanical stretch filament yarn, optimizing durability while preventing seam failure at stress points.
Field athletes experience intense body heat dissipation. By implementing engineered cross-section micro-denier fibers, our moisture transmission architecture pulls vapor rapidly toward the outer garment shell, facilitating lightning-fast evaporation during intense summer innings.
Bypassing trading houses and brokers cuts procurement markups by up to 35%. Direct-factory collaboration enables agile batch customization, precise inventory turnover ratios, and customized freight consolidation tailored to North American and European athletic clubs.
Using imported Swiss and Japanese disperse inks ensures deep color saturation resilient against high-UV baseball diamond conditions. Lab-certified colorfastness reaches Grade 4.5+ across standard industrial laundering and sweat-exposure wash tests.
Authentic baseball aesthetics necessitate precision zig-zag stitched tackle twill lettering and multi-layered patches. Integrated 12-head embroidery suites execute complex multi-color cresting without compromising internal panel comfort or adding unnecessary bulk.
Elevate standalone apparel collections into high-value market assets. We supply heat-seal transfer neck tags, custom-woven crest labels, certified swing tickets, QR-enabled barcode stickers, and biodegradable polybag packaging tailored to drop-shipping and retail displays.
Global athletic organizations are actively setting carbon reduction milestones. In response, modern custom baseball apparel engineering is migrating toward post-consumer GRS-certified recycled polyester (rPET) blended with circular bamboo viscose. Choosing a manufacturing partner that implements closed-loop sublimation wastewater recovery guarantees regulatory compliance across North American and European environmental import directives.
Transparent benchmark capabilities governing production lines, quality gates, and shipping SLAs.
| Minimum Order Quantity (MOQ) | 20 pieces per design, flexible across full adult & youth size scales (XS to 5XL). |
|---|---|
| Lead Time & Production Cycle | Pre-production sampling: 3–5 working days. Bulk runs (under 1,000 units): 7–10 working days. Rush capacity protocols available upon request. |
| Fabric Compositions | Heavyweight interlock polyester, warp-knit double-knit mesh, nylon-spandex 4-way stretch panels, anti-microbial dri-fit jersey, and GRS-certified rPET. |
| Custom Decoration Processes | Full dye-sublimation printing, tackle twill appliqué, 3D silicone heat press, direct-to-film (DTF), and computerized high-speed multi-head embroidery. |
| Quality Assurance Protocols | Piece-by-piece dimensional tolerance checks (±0.5 cm), tensile seam elongation load checks, and pre-packing needle detection. |
| International Logistics | Direct air cargo (DHL/FedEx/UPS express, 3–5 day delivery) and consolidated sea freight (FCL/LCL) to 30+ destinations including the USA, UK, Canada, Australia, and EU. |
Critical market shifts corporate buyers, athletic directors, and team apparel brand owners must monitor for 2025–2030.
The era of holding vast, speculative bulk inventory is ending. Leading baseball leagues and universities favor agile micro-runs with instantaneous computerized roster variable adjustments (numbers, player surnames, sponsor badges) fulfilled on lean 7-day manufacturing cycles.
Modern uniform cuts move away from boxy, restrictive silhouettes toward bio-mechanical cuts. Underarm gussets, laser-cut ventilation zones, and articulated raglan sleeves enable maximum rotational torso extension for batters and unhindered shoulder mobility for pitchers.
Eliminate sampling waste and speed up decision-making. Brands now review photorealistic CLO3D rendered mockups for multi-panel color placement and embroidery texture maps, reducing approval cycles from several weeks to less than 48 hours.
Direct technical answers addressing minimum orders, fabric selection, logistics, and quality assurance.
Dealing directly with our manufacturing floor removes intermediary commissions, speeds up technical revisions, and gives buyers full clarity over fabric specs, sample testing, and delivery schedules.
We work with international Pantone (PMS) matching libraries alongside Spectrophotometer lab analysis. Whether transitioning between jersey interlock poly and cap cotton twill, our lab-dip approvals ensure unified team palettes across all garments.
Yes. Our low MOQ of 20 pieces per design supports full size integration across Youth (YXS–YXL) and Adult (S–5XL) patterns, providing startups and clubs an accessible avenue for custom team kit rollouts.
Our standard protocol includes physical pre-production sampling before cutting bulk lots. If fit alterations, logo repositioning, or thread changes are needed, updates are completed promptly and documented before mass cutting begins.
We generally operate on a 70% advance deposit to schedule production, with the remaining 30% balance settled upon final QC approval prior to dispatch. Standard options include Wire Transfer (T/T), PayPal, Payoneer, and Wise.
All raw textiles, non-toxic sublimation inks, and heat-applied decals comply with OEKO-TEX Standard 100 Class I/II specifications, guaranteeing garments are hypoallergenic and free from banned azo dyes, phthalates, and heavy metals.