Pro Training
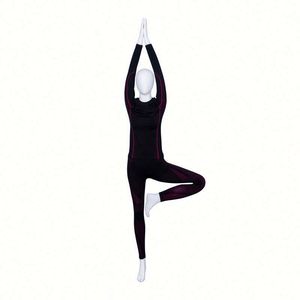
Wholesale Fitness Yoga Wear 2 Pcs Seamless Workout Yoga Gym Sport Suit
Seamless Knit
High Elasticity

Engineered directly in Sialkot, Pakistan—the sports goods capital of the world. Offering agile production, low 20-piece MOQs, and proprietary athletic fits.
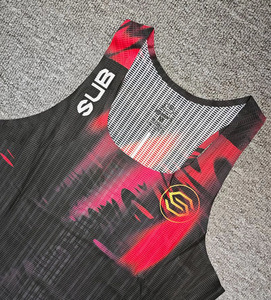
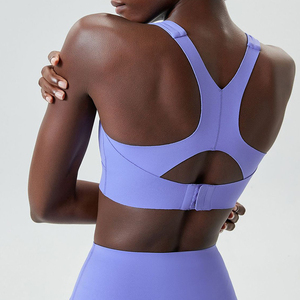
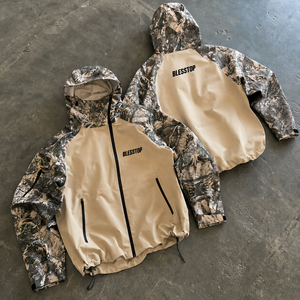
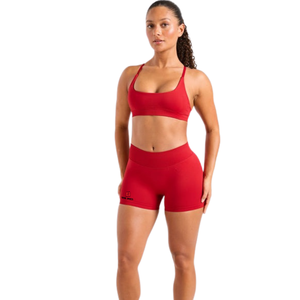
Combining Sialkot's century-old sports gear heritage with state-of-the-art Italian sublimation technology and transparent supply chain execution.
Zero intermediaries, agents, or trading house markups. You collaborate directly with our pattern cutters, embroidery technicians, and quality inspectors right in Sialkot, guaranteeing absolute cost efficiency and crystal-clear accountability.
Scale your cricket clothing brand without excessive capital exposure. We support startup athletic brands, franchise trial editions, and local premier clubs with full custom tailoring from just 20 pieces per design, scalable to 20,000 units.
Time to market is critical during league draft seasons. Orders under 1,000 pieces are completed within 7–10 business days post-sample approval, backed by dedicated air and ocean freight lanes serving 30+ countries including the UK, Australia, US, and UAE.
Zero batch surprises. Every cricket team uniform order initiates with an exact physical or expedited counter-sample. Cutting, panel sublimation, seam reinforcement, and sizing tolerances are confirmed in-hand before bulk production lines run.
Transform technical fabrics into retail-ready merchandise. We supply multi-head crest embroidery, silicone heat transfers, laser-cut ventilation eyelets, custom jacquard neck ribbing, woven size tags, and barcoded biodegradable polybags.
Headed by Chief Executive Officer Muhammad Pervaiz in Sialkot, with dedicated corporate liaison representatives Johnny Johnson in North America and Sheikh Nisar in Japan. We eliminate communication lag and understand cross-border compliance.
A comprehensive technical overview for brand directors, commercial buyers, and equipment managers procuring professional match-day whites, T20 color apparel, and training teamwear.
Global sports governing bodies and premier leagues are aggressively enforcing ESG mandates across teamwear procurement. In cricket apparel manufacturing, standard virgin polyesters are rapidly being phased out in favor of GRS-certified recycled polyethylene terephthalate (rPET), derived from post-consumer plastic bottles. Sourced directly from certified filament extruders in the Punjab industrial hub, our rPET yarns deliver tensile strength parity (4.2–4.8 g/denier) with conventional synthetic fibers while reducing manufacturing carbon emissions by 42%. Combined with non-toxic, water-based Oeko-Tex Standard 100 sublimation dyes, modern cricket kits maintain luminous chromatic intensity across 50+ industrial washes without releasing microplastic pollutants.
Cricket involves explosive asymmetric biomechanics: fast bowlers experience high thoracic velocity during delivery strides, while batsmen endure prolonged thermal traps under high midday solar indices. Next-generation cricket uniform engineering relies on body-mapped zoned jacquards. By pairing 135 GSM micro-diamond pique panels across the chest and thighs with ultra-light 95 GSM elastane eyelet mesh along the axillary vents, latissimus dorsi, and groin, core body temperatures drop by an average of 1.4°C during 5-day Test match play. Ergonomic raglan sleeves eliminate seam abrasion under heavy protective chest and shoulder armor, allowing unrestricted bowling actions.
| Discipline | Standard Fabric Composition | Fabric Weight | Surface Engineering | Recommended Decoration Method |
|---|---|---|---|---|
| Test & First-Class Match (Traditional White/Cream) | 92% Micro-Polyester / 8% Spandex Interlock | 200–220 GSM | UPF 50+ Sun Shield, Hydrophilic Soil-Release Finish | High-Definition 3D Silicone Crest & Direct-to-Garment Woven Embroidery |
| T20 / Hundred / Franchise League Colorwear | 100% Recycled Poly Mini-Pique / Micro-Mesh Zoned | 155–170 GSM | Quick-Dry Capillary Wicking, Dynamic 4-Way Stretch | All-Over Digital Italian Sublimation (Fluorescent / CMYK Pantone Validated) |
| ODI Teamwear & Training Warmup Pants | 88% Polyester / 12% Lycra Stretch Twill & French Terry | 240–260 GSM | Anti-Pilling, Brushed Internal Fleece, Water-Resistant DWR Coating | Reflective 3M Heat Transfer, Laser-Bonded Zip Pockets |
| Slip Fielders & Keeper Baselayers | 85% Polyamide (Nylon 6.6) / 15% Elastane Compression | 180–190 GSM | Graduated Targeted Compression, Antimicrobial Silver-Ion Finish | Flatlock 6-Thread Anti-Chafe Seams, Sublimated Monograms |
Key directives shaping athletic supply chains, international trade regulations, and brand customization strategies over the next five years.
Traditional athletic brands historically faced immense inventory risk by committing to 5,000-piece production runs before team trials concluded. The modern paradigm leverages digital micro-factories. With modular setups like ALEZ Industry's 20-piece MOQ framework, clubs can test seasonal variations, introduce limited-edition merchandise, and reorder exact quantities with zero warehouse stagnation.
Elite international teams increasingly monitor athletic strain, heartbeat metrics, and bowler shoulder torque using internal fabric sensor pockets. Uniform architectures now incorporate non-restrictive, bonded interior neoprene chassis to stabilize micro-GPS pods between the scapulae, demanding flawless technical stitching that resists high centrifugal forces without player distraction.
Supply chain shocks have prioritized direct-factory shipping over complex multi-warehouse re-routing. With Sialkot's dedicated international air cargo hub and streamlined export clearing corridors to Karachi Port, cricket brands in Europe and Australasia consistently achieve 4-to-6 day DHL Express delivery windows for urgent mid-tournament roster replenishments.
Practical commercial, technical, and regulatory answers addressing the primary pain points of corporate sportswear importers.
ALEZ Industry is an incorporated, 100% factory-direct manufacturer located at Bismillah Chowk, Pasrur Road in Sialkot, Pakistan. All core production stages—including computerized pattern grading, sublimation plotting, heat press transfer, 12-head embroidery, four-needle flatlock stitching, and AQL 2.5 final inspection—are executed in-house by our full-time workforce of 100+ skilled artisans. We welcome pre-scheduled on-site audits and live video facility walkthroughs.
Our minimum order quantity (MOQ) is strictly 20 pieces per design. Within this 20-piece allocation, clients are free to distribute mixed sizing (e.g., Small, Medium, Large, XL, Youth sizes) to accommodate realistic squad requirements. This low entry threshold enables athletic startups, schools, and local tournament franchises to secure professional-grade apparel without tying up working capital.
We utilize calibrated high-resolution sublimation printers paired with high-purity European disperse inks. Color matching is standardized using the Pantone Matching System (PMS Formula Guide Solid Coated). Prior to bulk garment assembly, digital swatches and physical lab-dips undergo spectrophotometer inspection under D65 artificial daylight settings to eliminate metamerism and maintain delta-E tolerances below 1.0 across seasonal runs.
Standard counter-sample fabrication requires 3–5 business days. Once the physical sample is approved by the client, bulk production runs under 1,000 units are completed in 7–10 business days; volumes exceeding 1,000 units typically require 12–15 business days. International express transit (via DHL, FedEx, or air freight forwarders) takes an additional 4–7 business days to North America, the UK, Europe, and Australia.
Standard production terms require a 70% advance payment to trigger fabric allocation, sample development, and line scheduling, with the remaining 30% balance plus freight settlement due upon quality sign-off before final factory dispatch. We accept secure commercial Bank Wire Transfers (T/T), PayPal for sample orders, Payoneer, Wise, and Western Union. Production is quoted primarily under FOB Karachi or Ex-Works (EXW) Sialkot, with DDP (Delivered Duty Paid) options available upon request.
Cricket trousers and sliding shorts undergo specific mechanical anti-abrasion testing. We reinforce lateral outer-thigh seams and knee zones using dense double-knit interlock structures with durable twin-needle coverseams. Our polyester fibers feature high tenacity filaments that resist friction-induced pill breakdown and turf burns on hard, dry outfield conditions.