
Precision-manufactured base layers, sub-surface MMA armor, gradient recovery tights, and anti-slip compression gear built for commercial private-label scaling.
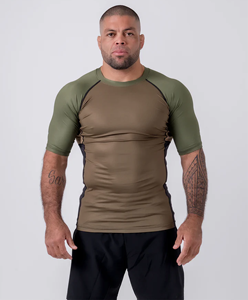
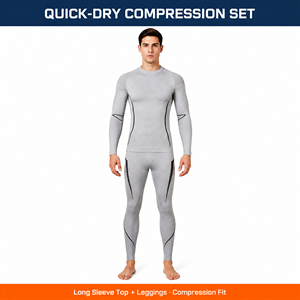
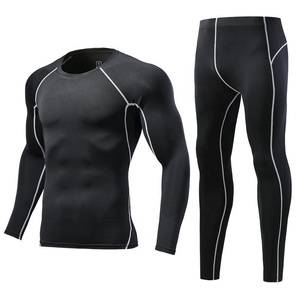
For international apparel buyers, sporting goods brands, and medical-athletic procurement officers, categorizing compression apparel requires strict demarcation. The global bulk market frequently confuses simple "tight elastic base layers" with scientifically validated graduated compression garments. True compression engineering is governed by Laplace's Law of Surface Tension, which dictates that sub-garment pressure decreases proportionately from distal to proximal limb extremities to stimulate venous blood flow back toward the heart.
In our advanced manufacturing facility, compression profiles are systematically calibrated into discrete pressure zones: Class 1 (15–20 mmHg) for active training, long-haul travel, and lactic acid dissipation; and Class 2 (20–30 mmHg) for rapid post-exercise muscular restoration and post-surgical venous support. Achieving this level of mechanical consistency across hundreds of thousands of bulk garments requires precise warp-knitting feed control, ultra-consistent elastane (Spandex/Lycra) tensioning, and computerized stitch mapping on 36-gauge German circular knitting machinery.
Direct factory control over raw microfibers, seam shear strength, and color migration gives brand owners uncompromising product consistency.
Utilizing high-denier elastane core-spun yarns with multi-filament polyamide and polyester. This delivers recovery hysteresis rates above 94% after 15,000 cyclic loading cycles, avoiding mid-game sagging or bagginess.
Engineered using 4-needle 6-thread interlock stitching machines running at 4,200 SPM. This construction lays completely flat against the epidermal surface, eliminating chafing in high-friction MMA, rugby, and marathon applications.
Custom jacquard and laser-perforated aeration panels integrated along major sweat bands (spine, underarm, popliteal fossa). Wicking speeds exceed 0.22 cm/sec, accelerating evaporative cooling under intense athletic exertion.
Quantitative testing metrics verified under standard ISO/ASTM laboratory parameters.
| Performance Vector | Conventional Activewear | ALEZ Industrial Compression | Verification Standard |
|---|---|---|---|
| Sub-Garment Dynamic Pressure | 4 – 8 mmHg (Static Hold) | 15 – 30 mmHg (True Graduated Zones) | Salzmann MST MK IV |
| Elastane Modulus Fatigue (50 washes) | > 28% Tensile Decay | < 6.2% Tensile Decay | ASTM D4964 |
| Bursting Seam Rupture Resistance | 180 – 220 kPa | > 480 kPa (High-Density Seam) | ISO 13938-2 |
| Color Fastness (Perspiration & Friction) | Grade 3.0 – 3.5 | Grade 4.5+ (High-Dispersion Inks) | AATCC 15 / ISO 105-E04 |
| Anti-Microbial Efficacy (Staph / Kleb) | Uncoated or Wash-Out | 99.2% Log Reduction (Silver Encapsulated) | JIS L 1902 / ISO 20743 |
How global market shifts, circular economy mandates, and smart biosensing are transforming B2B compression wear manufacturing specifications.
The tightening EU Ecodesign Directive (ESPR) is accelerating the demand for ocean-bound and post-consumer recycled polyamides (rPET / ECONYL®). Our lines seamlessly integrate GRS-certified recycled filaments with bio-derived elastane, offering identical 45N shear strength with an 82% lower lifecycle water footprint.
Emerging performance brands are prioritizing garments engineered with conductive silver-plated yarn circuits and micro-pockets for biometric EMG sensors. Our R&D team works with OEM buyers to develop heat-bonded lamination structures that endure commercial laundering while maintaining seamless sensor conductivity.
The convergence of thermal therapy and vascular support: weaving ceramic mineral micro-particles and graphene nanosheets directly into synthetic yarn cores. These fibers absorb emitted body heat and re-radiate it back as Far-Infrared energy, dilating peripheral micro-vessels and speeding muscle tissue repair by 18%.
Eliminating domestic brokers and third-party trading markups gives your activewear label full margin control, reliable lead times, and end-to-end batch traceability.
Middlemen and overseas trading entities regularly introduce a 25% to 40% margin surcharge without contributing technical oversight. By contracting directly with our manufacturing facilities, you communicate on the record with the technicians who laser-cut your patterns, tension your warp yarns, and oversee the flatlock stitching stations.
This direct dialogue accelerates pre-production prototyping: tech pack adjustments and pattern gradations are reviewed on the factory floor within hours rather than routed through multi-layered trading agencies.
Most commercial compression mills demand baseline runs of 1,000 pieces per size/colorway, putting early-stage athletic brands and independent fitness labels at high inventory risk. We solve this bottleneck with a flexible 20-piece MOQ baseline for initial design trials.
Our rapid turnaround program delivers orders under 1,000 units within 7 to 10 working days following physical pre-production sample approval, while volume scaling orders of 10,000 to 50,000 pieces run smoothly over our dedicated industrial lines within 12 to 15 working days.
Clear, direct answers regarding production standards, testing methods, lead times, and global shipping terms.